





Key Design Factors That Affect Dry Bulk Storage Tank Safety and Material Discharge Stability
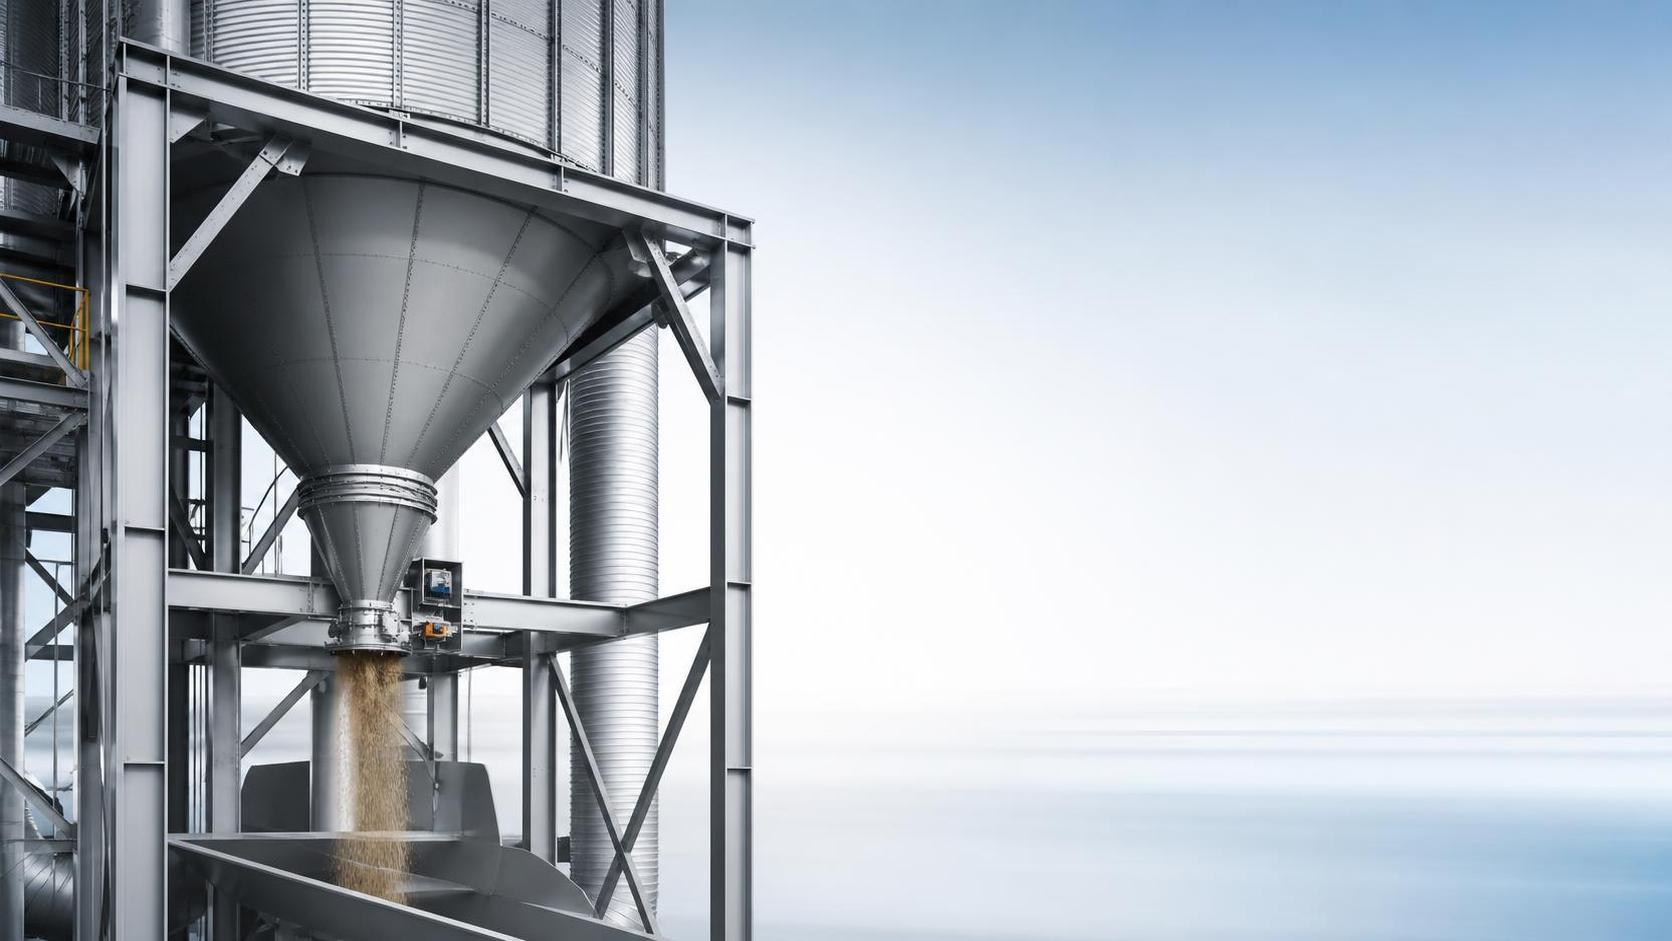
Why safety problems in dry bulk tanks often begin as design problems
A dry bulk storage tank is rarely judged by its shell alone. In practice, safety and discharge stability depend on how the structure, the stored material, and the discharge system behave as one system. That is the point many projects miss. A tank may look adequately sized, use compliant steel, and still create chronic arching, erratic flow, high wall loads, dust leakage, or even local structural distress if the design assumptions do not match the actual bulk solid.
For quality control and safety management teams, this matters because many incidents are not caused by a single dramatic defect. They build up from small mismatches: a hopper angle that is acceptable for one powder but not another, a venting arrangement that cannot keep pressure balanced during pneumatic filling, a discharge opening sized for nameplate throughput rather than real flow properties, or a transition detail that concentrates stress where material flow is already unstable. In dry bulk storage tanks, the line between “works most of the time” and “creates a recurring risk” is often drawn by design detail.
The right way to read a tank design is not to ask whether it can store material. Almost any vessel can do that. The better question is whether it can store, protect, and discharge a specific bulk solid repeatedly without creating unsafe loads, contamination, segregation, or manual intervention.
Flow behavior is the real starting point
When engineers talk about dry bulk handling, flow behavior usually drives the rest of the design. Powders and granules do not act like liquids, and two materials with similar bulk density may discharge very differently. Moisture sensitivity, particle shape, consolidation tendency, cohesion, particle size distribution, and aeration behavior all change how material moves inside the tank.
This is why outlet geometry and hopper design deserve more attention than they often receive. A common mistake is treating discharge problems as operational issues only. Teams install vibrators, air pads, or manual poking routines after startup, when the underlying problem is usually geometric. If the outlet is too small or the hopper is too shallow for the material’s flow characteristics, flow aids may reduce symptoms but not remove the root cause. They can also introduce new issues such as segregation, inconsistent feed, or localized wear.
In broad terms, designers usually think in terms of funnel flow and mass flow. Funnel flow can be acceptable in some duty conditions, but it tends to leave stagnant zones and can increase the risk of ratholing, caking, and product age variation. Mass flow is generally preferred where stable first-in-first-out movement, reduced residue, or sensitive materials are important. That does not mean every tank must be designed for idealized mass flow; it means the flow pattern should be chosen deliberately, with a clear understanding of what the material can tolerate and what the process requires.
Structural safety is tied to how bulk solids load the tank
Bulk solids apply loads differently from liquids, and uneven flow can make those loads less predictable. During filling, discharge, eccentric withdrawal, or temporary blockage, wall pressures may not remain symmetrical. That is one reason discharge instability is not just a productivity issue; it can become a structural issue.
The shell, stiffeners, roof, hopper, support frame, and transition zones should be assessed as load-bearing parts of one assembly. Particular attention usually goes to the junction between cylindrical walls and conical or pyramidal hoppers, as well as support connections and nozzle penetrations. These areas see stress concentration and are also where poor fabrication tolerance can magnify design weakness. In sectors such as grain, cementitious materials, power plant additives, or chemical powders, filling and emptying cycles are frequent enough that fatigue and repeated local stress should not be treated casually.
This is where manufacturing discipline becomes part of safety performance. A technically sound drawing loses value if weld quality, fit-up accuracy, corrosion protection, or bolt installation are inconsistent. Companies engaged in steel silo development and construction, including suppliers serving grain, building materials, electric power, and chemical applications, usually learn the same lesson over time: the tank is only as reliable as the coordination between design assumptions and fabrication control.
Sealing, venting, and dust control are not secondary details
Another frequent misunderstanding is that sealing performance is mostly about keeping material dry. That is only part of the story. Poor sealing can allow moisture ingress, yes, but it can also affect dust release, pressure balance, housekeeping burden, corrosion rate, and even the consistency of stored product where environmental exposure matters.
For dry bulk storage tanks filled pneumatically or at high throughput, vent sizing and filtration arrangement are critical. Inadequate venting can create pressure excursions during filling, while poor dust collection layout can shift fine particles into unwanted areas or overload filters. If the material is combustible in dust form, the design review has to consider the relevant explosion protection strategy for the jurisdiction and application. That review normally extends beyond the vessel body to include vents, ducts, valves, and housekeeping around transfer points.
Quality teams often catch the warning signs early: unusual dust traces near roof seams, seal wear around access points, repeated filter blinding, or unexplained moisture variation in the discharged product. Those are not cosmetic problems. They are indicators that the tank may not be operating within the assumptions used when it was selected or built.
Material discharge stability depends on consistency, not just flow rate
Stable discharge means more than “material comes out.” In many plants, the real requirement is controlled, repeatable discharge into downstream equipment such as feeders, mixers, mills, dosing lines, or pneumatic conveyors. A tank that empties in surges can upset the entire process even if it never fully blocks.
Several design factors interact here:
Notice that none of these are isolated features. A well-sized outlet can still perform badly if the feeder draws material unevenly. A polished hopper lining may not solve a powder that is compacting under residence time. Stability comes from matching the whole discharge path to the material and operating pattern.
Residence time, segregation, and contamination deserve more scrutiny
In quality management, storage safety is often discussed in terms of failure prevention, but material quality loss can be just as serious. Long residence time in stagnant zones may encourage caking, moisture pickup, oxidation, or temperature-related degradation, depending on the product. Segregation is another recurring problem, especially where the bulk solid contains a wide particle size distribution. Material may separate during filling and then discharge inconsistently, creating process variation batch after batch.
The design implication is straightforward: internal geometry should be reviewed for how it influences both flow pattern and cleanout. Access points, inspection doors, and maintenance strategy matter because residual material is rarely harmless. In food-adjacent, chemical, and mineral applications alike, contamination risk often grows in areas that were awkward to inspect from the start.
This is one reason equipment buyers sometimes compare adjacent storage categories. A facility planning mixed liquid and dry material handling may source both dry bulk vessels and products such as Oil Storage Tanks, but the inspection logic is different. Liquid containment priorities tend to center on leakage and corrosion pathways, while dry bulk containment adds flow pattern, dust behavior, and discharge mechanics as daily operational concerns.
How to judge a design without treating every supplier claim as equal
A useful review starts with questions that force the design back to operating reality. What exact material or material range is expected? What are the credible variations in moisture, density, temperature, and particle size? Is the tank meant for buffer storage, long residence storage, or continuous day-to-day cycling? How is the material introduced, and what equipment withdraws it? Has the design accounted for asymmetric flow or upset conditions, not just ideal filling and emptying?
Then look for evidence of engineering discipline rather than broad promises. For example, was the discharge section selected from tested flow properties or simply copied from a prior project? Are support details and wall thickness choices tied to recognized design methods and applicable codes? Are sealing details, venting provisions, access arrangements, and corrosion protection described clearly enough to inspect later? A serious supplier should be able to explain these choices in operational terms, not just list materials and dimensions.
That same discipline applies when a project spans several storage media. Even if a supplier portfolio includes items like Oil Storage Tanks, dry bulk tank evaluation should remain material-specific. Similar steel fabrication capability does not automatically mean similar performance under powder flow conditions.
Where quality and safety teams should focus during acceptance and operation
Once the tank reaches site, acceptance should cover more than dimensional conformity. Verify critical fabrication details, weld condition, coating integrity, bolted connections, alignment of discharge components, and the actual arrangement of vents, level instrumentation, and access hardware. If the project includes liners, flow aids, or special feeder interfaces, those should be checked against the design intent, not merely for presence.
During operation, trend the symptoms that usually precede larger failures: increased bridging frequency, rising manual intervention, uneven feeder loads, recurring dust escape, abnormal vibration use, accelerated wear at transitions, or product quality drift linked to storage time. These indicators often show that the design margin is being consumed by changes in material condition or throughput demand.
The practical lesson is simple. Dry bulk storage tanks should be judged as process equipment with structural consequences, not as passive containers. If the design reflects real bulk material behavior, the tank is easier to operate safely and easier to keep within quality limits. If that behavior is guessed at or oversimplified, the plant usually pays for it later in blockages, dust, unstable discharge, and avoidable maintenance risk.
Related Posts
- ▶ How a Dry Bulk Silo Handles Pneumatic Filling and Gravity Discharge
- ▶ What Is a Dry Bulk Silo, and When Does a Factory Need One?
- ▶ Can dry bulk storage silos be integrated into existing PLC-controlled batching systems?
- ▶ Do dry bulk silos designed for API 650 compliance meet ASME Section VIII requirements?
- ▶ Is almacénamiento de sólidos a granel en silos de acero inoxidable viable for small-scale agrochemical distributors?
- ▶ How do vibration-based level sensors perform in stainless steel silos with powder coating?
Online Message