





How to prevent bridging and rat-holing in stainless steel silos storing fine powders?
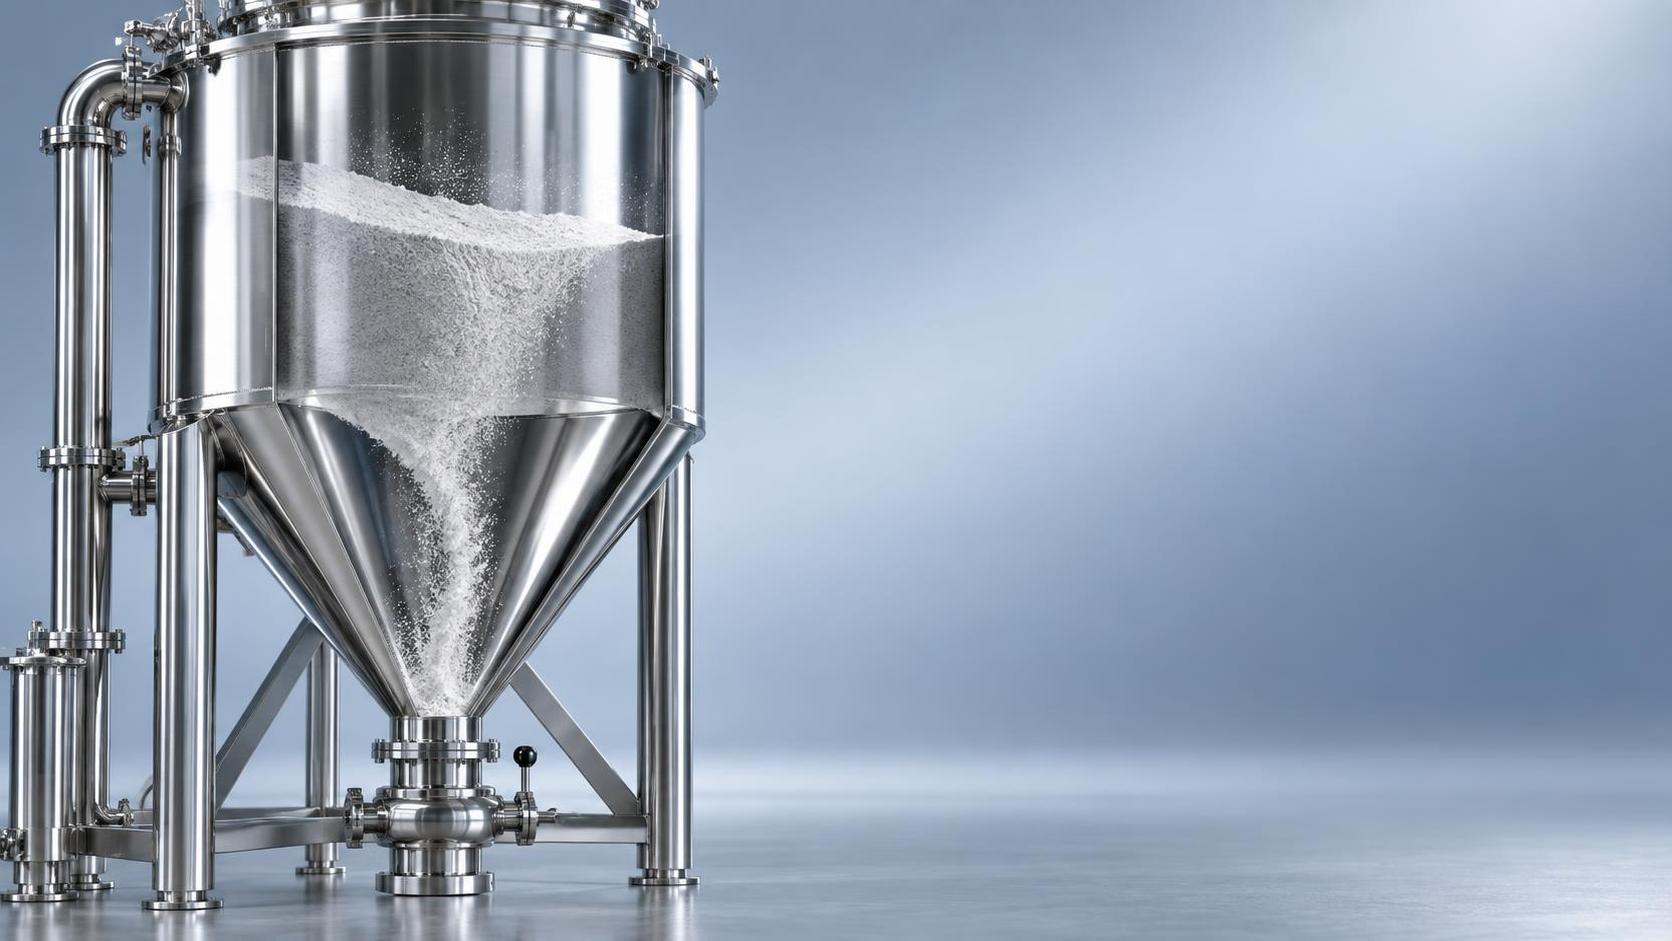
Bridging and rat-holing are not merely operational inconveniences—they represent material flow failures rooted in the interplay between powder rheology, stainless steel silo geometry, and discharge dynamics. Fine powders—especially those with high cohesion, low permeability, or moisture sensitivity—exhibit pronounced arching tendencies when stored in vertical cylindrical silos. Bridging occurs when a stable arch forms across the hopper outlet, completely halting discharge; rat-holing arises when only a narrow central channel flows while stagnant material adheres to the walls, progressively reducing effective capacity and increasing segregation risk. Both phenomena escalate under static storage conditions, temperature fluctuations, or minor vibration-induced compaction—common in grain, chemical, and power industry applications where stainless steel silos are specified for corrosion resistance, hygiene, or regulatory compliance.
Material Behavior Dictates Design Constraints
Stainless steel silos do not cause bridging—but their smooth, non-porous surfaces amplify the consequences of poor material handling. Unlike carbon steel or concrete, stainless steel offers minimal wall friction, which can delay initiation of flow but also reduce wall shear support once flow begins. For fine powders (e.g., alumina, titanium dioxide, or pharmaceutical excipients), particle size distribution below 50 µm, moisture content above 0.3%, or specific surface area exceeding 5 m²/g significantly increases cohesive strength. These properties directly influence the critical hopper angle required for mass flow: a powder with internal friction angle of 45° may require a hopper wall angle steeper than 60° relative to horizontal—even in stainless steel—to ensure consistent first-in-first-out discharge. Relying on generic “stainless steel silo” design templates without powder-specific flow testing risks undersized hoppers or inadequate outlet diameters.
Hopper Geometry: Beyond Minimum Angle
Simply meeting the theoretical hopper angle is insufficient. Real-world stainless steel silos must account for weld seam roughness, surface finish (typically Ra ≤ 0.8 µm for food-grade 316L), and localized cold-working during fabrication that alters local yield stress. A 65° conical hopper may still bridge if the transition radius between cylinder and cone exceeds 150 mm—creating a stagnation zone where powder consolidates under load. In practice, sharp transitions (radius ≤ 50 mm) combined with polished interior welds reduce dead zones. For ultra-fine powders, transition hoppers—featuring a shallow conical section followed by a steep conical or wedge-shaped discharge section—demonstrate superior performance over single-angle cones. The wedge design applies asymmetric pressure gradients that disrupt arch formation more effectively than symmetrical geometries, especially when paired with uniform wall thickness (≥6 mm for diameters >3 m) to minimize flex-induced pulsation.
Vibratory Assistance: Timing and Amplitude Matter
External vibrators mounted on stainless steel silo walls are common—but misapplication worsens rat-holing. Low-frequency, high-amplitude vibration (e.g., 10–30 Hz) applied continuously induces particle rearrangement that strengthens arches rather than breaking them. Effective vibration targets *only* during discharge initiation and uses short-duration, high-frequency pulses (40–120 Hz) timed to coincide with natural resonance frequencies of the filled hopper section. Mounting location is critical: vibrators placed at the cone apex generate radial energy most efficiently, whereas side-mounted units often transmit energy poorly through thick stainless walls. For silos storing hygroscopic powders, vibration must be synchronized with humidity-controlled purge air to prevent re-compaction post-activation.
Air-Assisted Discharge: Pressure, Not Volume
Pneumatic assistance is frequently misunderstood as “more air = better flow.” In stainless steel silos, excessive air volume creates fluidization channels that accelerate rat-holing by eroding central pathways while leaving peripheral material intact. Successful air-assisted systems use controlled, intermittent injection (0.5–2 bar gauge) through porous sintered stainless steel pads installed along the hopper walls—not at the outlet. These pads release air tangentially, generating gentle wall shear that loosens adhered layers without disturbing bulk density. Air injection timing must be phased: initial burst at start-up, then reduced pulses every 30–60 seconds during continuous discharge. Systems relying solely on bottom-air nozzles often fail because they bypass the wall-material interface where cohesion dominates.
Mechanical Agitators: When Rotation Isn’t Enough
Rotating paddles or helical blades inside stainless steel silos require precise torque calibration. Over-torqueing fractures fragile agglomerates into dust that increases electrostatic charge and cohesion; under-torqueing leaves compacted rinds untouched. Blade geometry must match powder compressibility: flat paddles work for low-cohesion materials like dried silica, while serrated or stepped blades better penetrate cohesive layers typical of Alumina Powder Silos. Crucially, agitator shaft seals must withstand abrasive wear without introducing lubricant contamination—standard graphite-packed seals degrade rapidly with fine powders, necessitating double mechanical seals with inert gas purging.
Operational Protocols That Prevent Degradation
Flow problems rarely emerge from a single flaw—they accumulate across cycles. Daily practices matter: never refill a partially emptied silo without first clearing residual wall buildup, as new powder layers bond to old crusts via capillary condensation. During shutdowns longer than 8 hours, maintain slight positive pressure (5–10 mbar) with dry nitrogen to inhibit moisture ingress through expansion joints—particularly critical for 304 stainless in humid climates. Outlet valves should open fully before initiating discharge; partial opening creates velocity gradients that promote channeling. And crucially: avoid using compressed air lances for manual bridging removal. Direct jet impact fractures arches unpredictably, sending shockwaves that consolidate adjacent material into denser, harder-to-dislodge masses.
Verification Through Flow Testing
No stainless steel silo design should proceed without shear cell testing of the actual powder under simulated storage conditions—including temperature cycling between 15°C and 40°C and exposure to ambient humidity levels expected onsite. Bench-scale tests reveal whether flow function coefficients indicate funnel-flow dominance (risking rat-holing) or reliable mass-flow potential. Field verification requires monitoring discharge rate consistency across three consecutive 80%–100% fill cycles—not just a single test run. A deviation exceeding ±12% in mass flow rate signals unresolved geometric or surface interaction issues, even if visual inspection shows no obvious bridging.
Preventing bridging and rat-holing in stainless steel silos demands treating the system as an integrated unit—where powder behavior defines structural requirements, surface properties modulate energy transfer, and operational sequencing determines long-term reliability. There is no universal angle, vibration setting, or air pressure; each solution emerges from the specific intersection of material, metallurgy, and process duty.
Related Posts
- ▶ How a Dry Bulk Silo Handles Pneumatic Filling and Gravity Discharge
- ▶ What Is a Dry Bulk Silo, and When Does a Factory Need One?
- ▶ Can dry bulk storage silos be integrated into existing PLC-controlled batching systems?
- ▶ Do dry bulk silos designed for API 650 compliance meet ASME Section VIII requirements?
- ▶ Is almacénamiento de sólidos a granel en silos de acero inoxidable viable for small-scale agrochemical distributors?
- ▶ How do vibration-based level sensors perform in stainless steel silos with powder coating?
Online Message