





Fly Ash Storage Options for Power Plants: Silo Design, Handling, and Dust Control
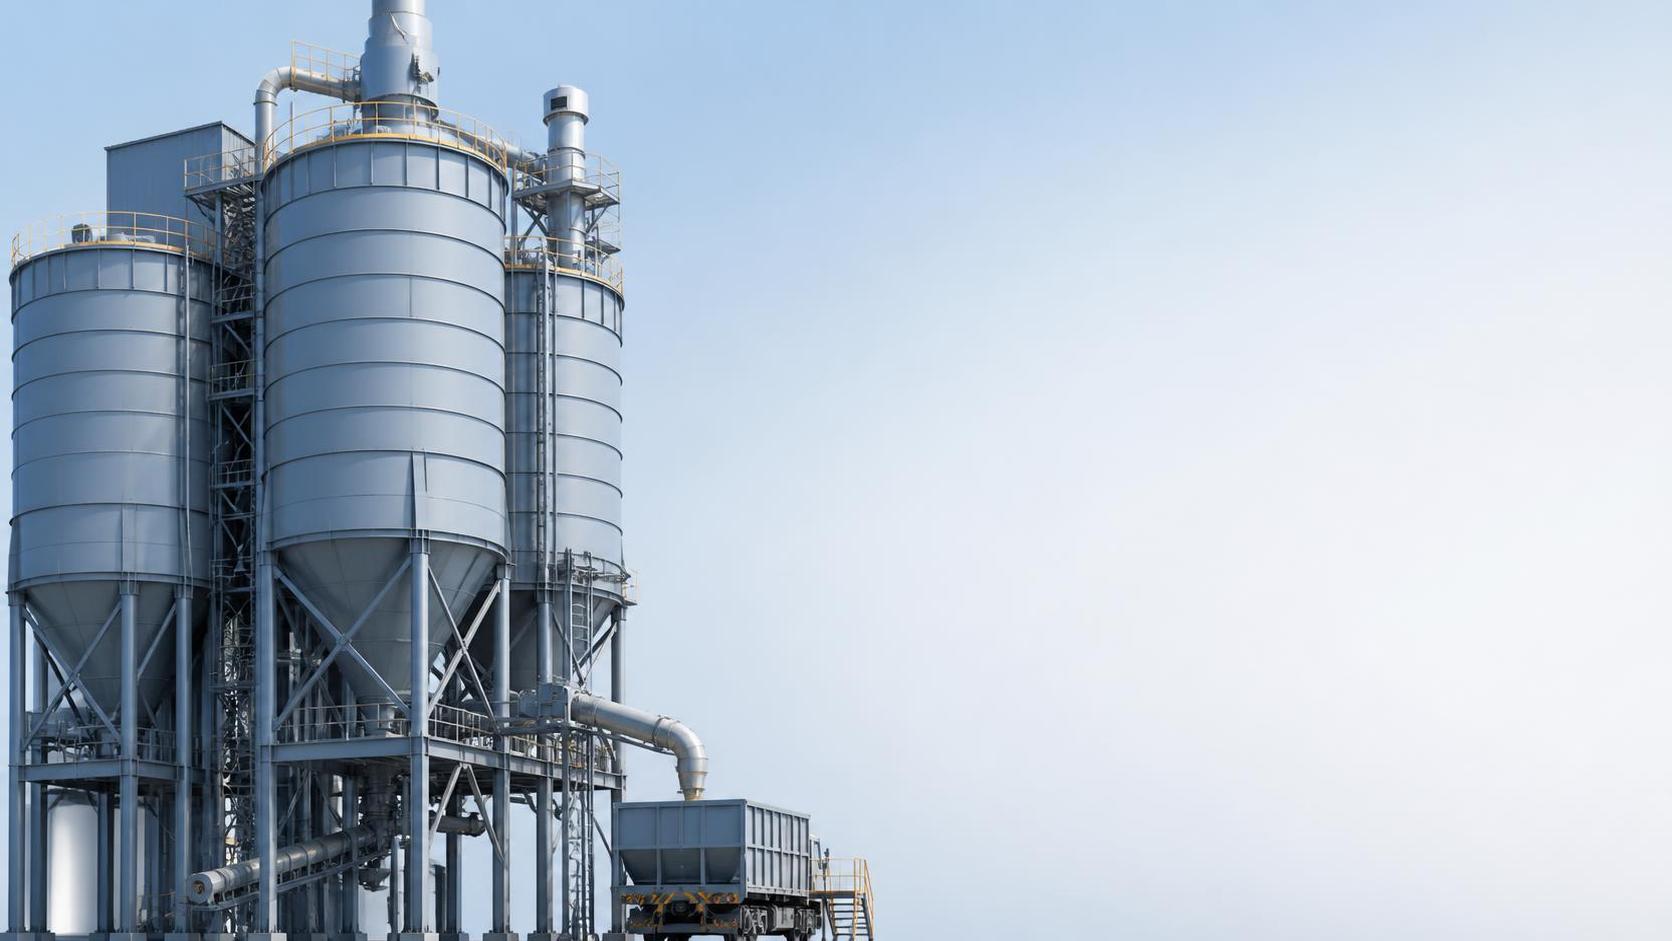
Start with the ash, not the silo drawing
Most fly ash storage problems begin before fabrication. A project team picks a silo size, adds a conveyor and a dust collector, then discovers later that the ash does not flow as expected, the unloading rate is unstable, or the roof venting is undersized for the way the system is actually operated. If you are managing a power plant project, the useful checklist starts with material behavior and operating rhythm, because those two things drive nearly every design decision that follows.
Fly ash storage is not just about holding volume. You are dealing with a fine powder that can bridge, compact, fluidize, leak through poor seals, and create persistent dust issues if one part of the system is out of balance. A well-built steel silo can solve a lot, but only when the discharge method, feeding mode, dust control, maintenance access, and operating limits are treated as one package.
The practical checklist project managers should run
Use this sequence when comparing fly ash storage options or reviewing a supplier proposal.
- Define the real storage duty. Separate daily balancing storage from emergency reserve storage. Those are not the same job. If the silo only buffers a few hours of ash before transfer, the filling and discharge frequency matters more than long-term compaction risk. If the silo may hold ash for extended periods, you need to pay more attention to aeration, discharge geometry, moisture exposure, and access for cleaning.
- Check ash source variability. Ask whether the ash comes from one unit or multiple units, and whether collection conditions change with fuel mix, load swings, or emissions equipment operation. Fine, dry ash from one operating mode can behave very differently from ash produced during another. A storage system that works in steady lab assumptions may become difficult to empty in real plant conditions.
- Confirm how the ash enters the silo. Pneumatic conveying, mechanical conveying, and truck loading all create different pressure and venting demands. Teams often focus on silo shell strength and forget the fill event itself. Overpressure during loading, especially when filters blind or venting is too small, is one of the avoidable failures you want off the table early.
- Decide what “empty” really means. Some projects accept a working heel of material in the cone; others need near-complete discharge because product segregation, hardening, or changeover matters. This affects hopper angle, outlet sizing, aeration arrangement, and whether you need mass-flow-oriented design principles rather than a simpler funnel-flow setup.
Silo sizing is more than a volume calculation
A common mistake is to size storage only from tons per day. For fly ash, you also need to look at filling peaks, truck dispatch windows, unplanned outage scenarios, and whether downstream users pull material continuously or in batches. A silo that is “big enough” on paper may still create operational dead time if the discharge system cannot keep up with demand during a short loading window.
At review stage, ask these questions:
- Is the working capacity based on bulk density assumptions that match the actual ash condition expected on site?
- Does the proposal distinguish between geometric volume and usable volume?
- How much buffer remains if truck loading is delayed, a conveying line trips, or one discharge point is unavailable?
- Will the chosen height and diameter fit erection constraints, access roads, crane use, and the plant layout around existing structures?
That last point gets missed more often than it should. A theoretically efficient silo is still a bad choice if the site cannot install or maintain it without disrupting the plant.
Pay close attention to hopper and discharge design
If a fly ash silo gives trouble, the discharge zone is usually where it starts. This is where flow pattern, aeration, arching risk, and wear all meet. Project teams sometimes treat the cone, outlet, valve, and feeder as standard items. They are not.
The practical review points are straightforward:
- Is the hopper geometry suitable for fine powder discharge, not just coarse bulk solids?
- Has the outlet been sized with the selected feeder or valve in mind?
- Are aeration pads or fluidizing elements placed where they help flow, rather than masking a poor geometry choice?
- Can the discharge equipment be isolated and serviced without putting the whole silo out of operation for too long?
One field lesson worth remembering: aeration is useful, but it is not a cure-all. If ash is repeatedly compacting, rat-holing, or discharging unevenly, adding more air often turns one problem into another. You can end up with flushing, unstable flow, or dust release downstream.
Dust control has to be built into the process path
When teams say they need better dust control, they often mean one of three different things: visible dust at truck loading, pressure release during filling, or housekeeping dust around valves and transfer points. Those are related, but not identical, and the fixes are different.
The cleaner systems are usually the ones where the engineer followed the material path from inlet to final discharge and closed every place where pressure and fine particles can escape together.
Do not separate structural durability from operating conditions
Power plant environments are demanding. Outdoor exposure, repeated pressure cycles, abrasive dust, and maintenance traffic all affect long-term performance. A steel silo supplier with real project experience in industrial storage will usually think beyond shell capacity alone and look at ladders, platforms, roof access, corrosion exposure, wear points, and how people will actually inspect the system after handover.
For project review, it helps to divide durability into four checks:
- Weather protection: keep moisture ingress under control at roof penetrations, manholes, and vent assemblies. Fly ash and unwanted moisture are a bad combination.
- Wear resistance: identify high-velocity inlet zones and abrasive discharge points early. That is where lining choices and replaceable components matter.
- Access: if filters, level devices, and valves cannot be reached safely, maintenance gets deferred, and deferred maintenance shows up later as dust, false readings, or blocked flow.
- Instrumentation protection: level switches, pressure indicators, and flow aids need installation positions that still make sense after months of dust exposure.
Match the storage option to the logistics around it
Not every fly ash project needs a large permanent silo as the only answer. During phased construction, temporary bypass operations, or satellite handling points, smaller mobile storage equipment can make sense around the edges of the main system. That is where something like Mobile Small Cement Tanks for Construction Site may fit as a support tool for nearby dry powder handling tasks, provided the duty and material compatibility are checked against the actual use case.
The point is not to force one piece of equipment into every job. The point is to review the whole handling route: main storage, temporary holding, truck loading, backup operation, and maintenance periods. Good project decisions usually come from that broader view.
Commissioning is where hidden design weaknesses show up
A fly ash silo can look complete and still be one bad startup away from a long punch list. Before handover, make sure the commissioning plan includes more than a no-load equipment rotation check.
- Test filling under realistic loading rates.
- Watch pressure behavior during loading and unloading, not just steady-state operation.
- Verify level measurement response when dust concentration is high.
- Check whether truck loading remains sealed when operators connect and disconnect in real site conditions.
- Confirm that the discharge system can restart cleanly after material sits idle.
Those last restart tests matter more than many teams expect. Fine powders behave differently after resting, especially if humidity, temperature swings, or compaction are part of the operating environment.
What usually gets missed in supplier comparison
When bids are close on price, compare the things that affect plant uptime later:
- How clearly the supplier defines the boundary between silo scope and auxiliary equipment scope.
- Whether the proposal addresses inspection access and replacement of wear parts.
- How the dust collection and pressure relief concept is described during the actual loading case.
- Whether discharge aids are integrated as a designed solution or added as generic accessories.
- How much operating information the supplier asks from you before finalizing the design.
That last one is a useful signal. A serious industrial silo partner will ask about material condition, loading method, discharge target, and site restrictions. If the questions are shallow, the design thinking behind the quotation may be shallow too.
A sensible action order for project teams
For power plant fly ash storage, the cleanest path is usually this: define the ash behavior and operating scenario, size the storage around actual logistics, lock down the discharge concept, then review dust control at every pressure transition point. After that, challenge access, maintenance, and restart performance before you approve the final package.
If one part still feels vague, do not let the project move forward on shell dimensions alone. In fly ash handling, the hard problems are rarely in the empty steel volume. They sit at the inlet, the cone, the venting path, and the day-to-day operating details that decide whether the system runs cleanly or keeps calling the maintenance team back.
Related Posts
- ▶ How a Dry Bulk Silo Handles Pneumatic Filling and Gravity Discharge
- ▶ What Is a Dry Bulk Silo, and When Does a Factory Need One?
- ▶ Can dry bulk storage silos be integrated into existing PLC-controlled batching systems?
- ▶ Do dry bulk silos designed for API 650 compliance meet ASME Section VIII requirements?
- ▶ Is almacénamiento de sólidos a granel en silos de acero inoxidable viable for small-scale agrochemical distributors?
- ▶ How do vibration-based level sensors perform in stainless steel silos with powder coating?
Online Message