





Dry Bulk Storage Tanks: Common Discharge Problems and How to Prevent Them
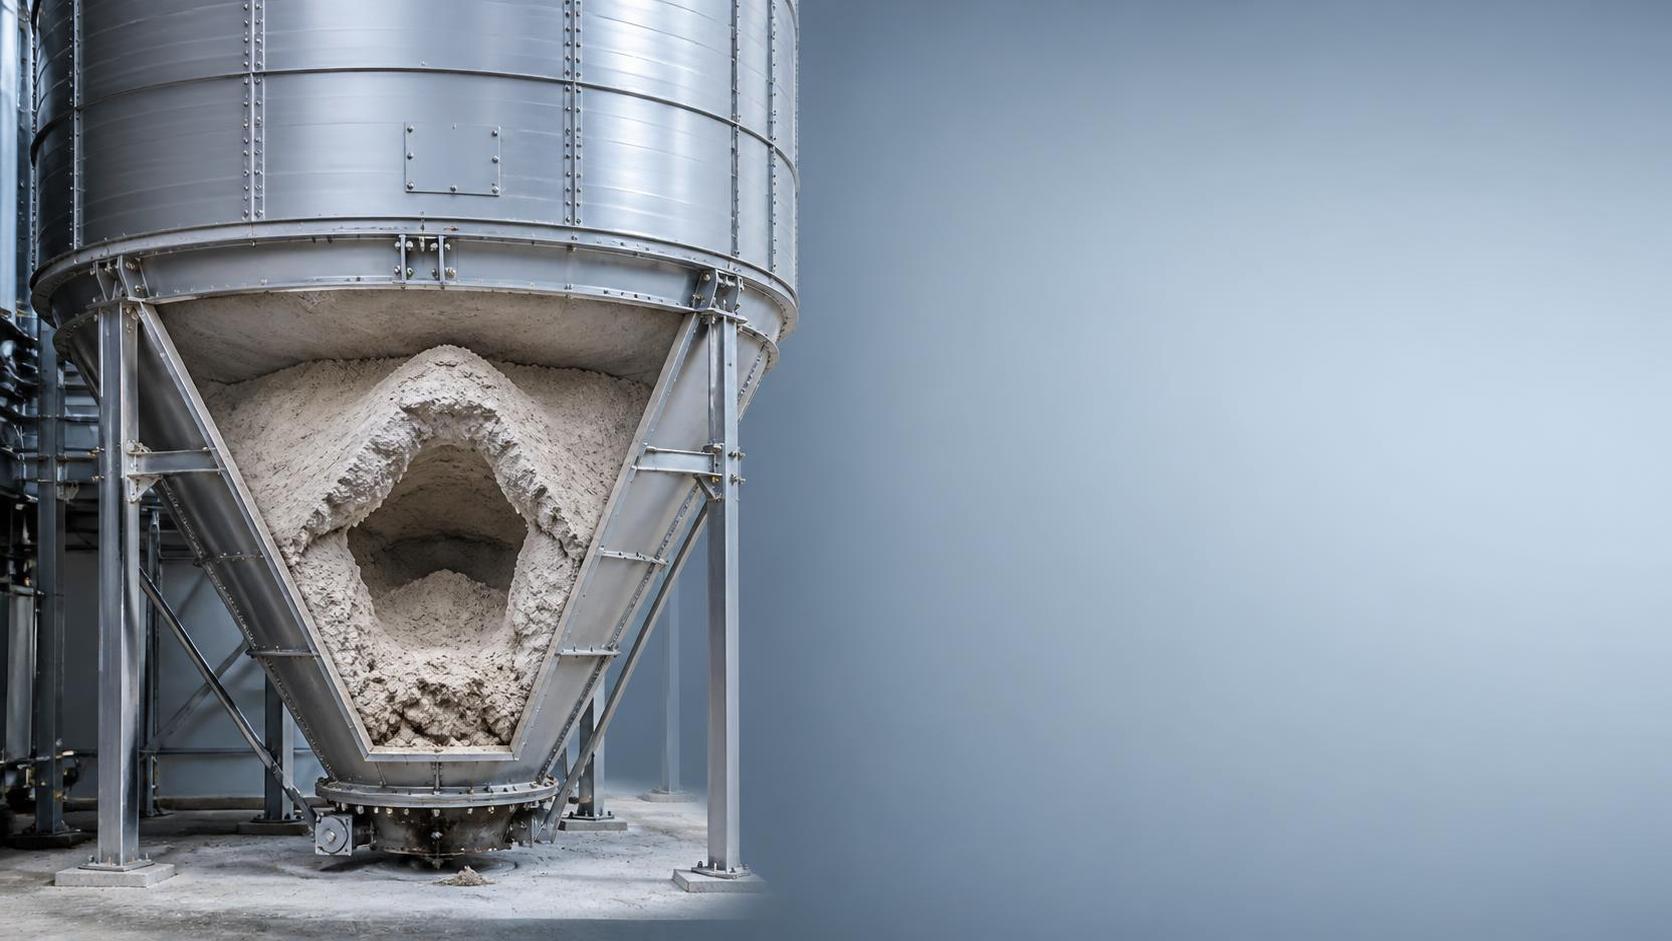
Dry bulk storage tanks are central to reliable material handling, but operators know that trouble usually starts at the discharge point. A tank may look structurally sound from the outside and still perform poorly when material refuses to flow, surges unexpectedly, or segregates during discharge. In practice, these problems do not come from one single cause. They usually result from the interaction of material behavior, tank geometry, discharge equipment, operating habits, and maintenance discipline.
In plants handling grain, cement, fly ash, lime, mineral powders, plastic resins, or chemical solids, discharge instability affects more than throughput. It can increase energy use, create quality variation, overload downstream equipment, raise dust exposure, and in severe cases introduce safety risks during manual intervention. For operators, the most useful question is not “what is the problem called,” but “why is this happening in this tank, with this material, under today’s operating conditions?”
The most common discharge problems in dry bulk storage tanks are usually recognizable: bridging, ratholing, erratic flow, flushing, segregation, and buildup around outlets or internal surfaces. Preventing them depends on early recognition and disciplined operating response rather than waiting for a complete blockage.
Bridging: when the material forms its own roof
Bridging occurs when bulk material arches across the outlet and creates a stable span that supports the weight above it. From the operator’s perspective, the tank appears full but discharge slows dramatically or stops completely. This is common in cohesive powders, damp materials, fine particles, and products that compact during storage.
Typical field signs include:
- discharge stops while level indication still shows inventory;
- vibrators or air pads seem to work only briefly;
- hammering the cone or outlet restores flow for a short time;
- flow interruptions become more frequent after humid weather or longer storage periods.
Bridging is often blamed on the tank alone, but operators should treat it as a system issue. The outlet may be too small for the material’s cohesive strength. Moisture pickup may be increasing lump formation. Pneumatic conveying fines may have changed the particle distribution. Repeated partial emptying may also compact material around the outlet over time.
Prevention starts with controlling what enters the tank. If the bulk solid arrives with variable moisture, temperature, or particle size, discharge problems are more likely no matter how robust the tank appears. During operation, avoid long idle periods with difficult materials if possible. Where stoppages are recurring, outlet design, hopper angle, and flow aids should be reviewed rather than relying on forceful manual clearing.
Ratholing: flow in the middle, stagnant material at the sides
Ratholing is different from bridging. Material continues to discharge, but only through a narrow channel above the outlet, leaving stagnant zones along the walls. Operators may notice an apparently normal discharge rate at first, followed by sudden collapse of the channel or a steep drop in flow as the active core empties.
This problem matters because stagnant material does not just reduce usable capacity. It can age, cake, absorb moisture, spoil, or contaminate later batches. In food, feed, fertilizer, and chemical service, that becomes a quality issue as much as a flow issue.
Ratholing is especially common when a tank operates in funnel flow rather than mass flow. In funnel flow, only the central channel moves first. In mass flow, material along the walls moves as well, which is usually preferred for difficult or degradable materials. Operators may not control the original design, but they can often identify operating conditions that worsen ratholing:
- consistent low withdrawal rates;
- frequent partial discharge cycles;
- material stored for too long;
- wall buildup increasing internal friction;
- changes in material properties that were not considered during setup.
If ratholing is recurring, the long-term fix may require reviewing hopper geometry or liner selection. In larger installations, especially where continuous process stability matters, tank design should match the real flow properties of the stored material rather than generic assumptions. This is one reason many industrial users evaluating mid- to large-capacity systems pay close attention to discharge configuration, not just storage volume, when specifying units such as 800-1500 Tons Silos.
Erratic flow and surging: when material does move, but not predictably
Not every discharge problem is a blockage. Some tanks empty in pulses. Material may hang up, release suddenly, then surge through the outlet. For operators, this is often more disruptive than a complete stop because it causes unstable feed to mixers, packing lines, screw conveyors, or pneumatic systems.
Erratic flow usually points to inconsistent de-aeration, non-uniform particle distribution, or unstable discharge assistance. Fine powders are especially sensitive. If material is highly aerated during filling and does not settle uniformly, it may initially flow too easily, then compact unpredictably. This can be seen in fly ash, cementitious materials, and some chemical powders.
Common triggers include:
- rapid filling followed by immediate discharge;
- excessive air injection near the outlet;
- poorly tuned rotary valves or screw feeders;
- inconsistent feeder speed control;
- segregated material with changing fines content near the outlet.
Prevention depends on stabilizing both the material condition and the withdrawal device. Operators should not assume the tank is at fault if the discharge feeder is fluctuating. In many plants, what looks like a silo problem is actually a metering problem downstream. Checking feeder load, motor current, and discharge rate trends often reveals whether the instability starts inside the tank or at the extraction equipment.
Flushing and flooding: too much flow, too fast
Some fine dry bulk materials do the opposite of bridging. Instead of resisting discharge, they flood. Material behaves almost like a liquid, resulting in uncontrolled high discharge rates, dust release, and difficulty in metering. This is often called flushing.
Operators typically encounter flushing after aeration, vibration, or filling conditions that leave the bulk solid highly fluidized. Fine, low-density powders are especially vulnerable. The danger is not only product loss or process upset. Overfeeding downstream equipment can cause line plugging, filter overload, or dust collector stress.
To reduce flushing risk:
- avoid over-aerating the material near the outlet;
- allow sufficient settling time where process conditions permit;
- check whether feeder design can handle fluidized material behavior;
- review venting performance, since trapped air can worsen instability;
- monitor any operational changes after material source or formulation changes.
A useful operator habit is to distinguish between “material won’t flow” and “material won’t meter.” The corrective actions are not the same, and confusing the two often leads to repeated troubleshooting without real improvement.
Segregation: the hidden cause behind inconsistent discharge
Segregation is often overlooked because the tank may discharge without obvious blockage. Yet when coarse and fine particles separate during filling, the discharge pattern changes over time. Early discharge may be rich in fines, later discharge coarse, or the opposite depending on filling method and material characteristics.
This creates two practical problems. One is process inconsistency: blend quality, moisture response, burn performance, or packaging weight can vary. The other is flow behavior itself. Segregated material can increase the risk of ratholing, flushing, or local compaction at the outlet.
Operators should be alert when a discharge problem appears after a change in filling practice, even if the tank hardware did not change. Central filling, off-center loading, drop height, and fill rate all influence segregation. If complaints include both poor flow and variable product quality, the root cause may begin during filling, not discharge.
Wall buildup, caking, and dead zones
Internal buildup gradually changes how dry bulk storage tanks behave. A tank that discharged well when new may become unreliable after months of residue accumulation. Sticky fines, humidity swings, temperature changes, and inadequate cleaning intervals all contribute.
Wall buildup matters for three reasons. It increases friction, reduces effective geometry, and creates intermittent release events when deposits break loose. These release events can damage feeders or contaminate product streams.
From an operational standpoint, a simple inspection routine often prevents larger problems. If safe access procedures are in place, monitor known buildup areas such as the cone, transition sections, and nozzles. Record when buildup forms, not just where. Timing often reveals the trigger: rainy season moisture, warm daytime/cool nighttime cycling, a new supplier lot, or longer holding times.
Why operators often misdiagnose discharge problems
One recurring issue in bulk solids handling is treating every flow problem as a mechanical fault. In reality, the same symptom can come from different causes:
- a blocked outlet may be caused by bridge formation, oversized lumps, or feeder back-pressure;
- slow discharge may come from compaction, feeder wear, air imbalance, or level measurement error;
- surging may be due to flushing, unstable feeder control, or partial collapse of a rathole.
This is why emergency measures such as external hammering or excessive vibration often create only temporary relief. They restore movement without correcting the reason movement stopped. In some cases, aggressive intervention can worsen structural fatigue, compact the material further, or create unsafe conditions for personnel.
Practical prevention steps that work in daily operation
For plant users and operators, prevention is usually less about one major modification and more about a set of consistent controls.
Track material variability. Record supplier changes, moisture shifts, and unusual particle behavior. If a discharge issue starts after a raw material change, that correlation is valuable.
Control filling practices. Uneven filling, high drop distances, and rapid loading can worsen segregation and aeration. Stable filling conditions often improve discharge consistency more than expected.
Do not ignore partial blockages. A tank rarely goes from normal operation to total failure without warning. Intermittent slowdowns, feeder load swings, and repeated manual assistance are early signs.
Verify feeder and outlet compatibility. The best-designed tank still depends on proper extraction equipment. Rotary valves, screws, slide gates, and air-assisted discharge devices must suit the actual material behavior.
Keep venting and air balance in check. Poor venting can trap air, affect pressure balance, and disturb discharge in fine powders.
Inspect for buildup and wear. Internal surfaces, liners, outlet transitions, and discharge aids should be reviewed before problems become chronic.
Use flow aids carefully. Vibrators, air cannons, and air pads are not universal solutions. Incorrect use may promote segregation, fluidization, or local compaction depending on the material.
When the problem points to design, not operation
Some discharge problems persist despite good operating practice. That usually means the issue is rooted in tank design assumptions that do not match the stored material. Outlet size may be inadequate. Hopper angles may be too shallow. Wall finish may create excessive friction. The selected flow pattern may not suit cohesive or degradable solids.
At that stage, repeated operational workarounds become expensive. Lost production time, labor intervention, quality losses, and maintenance costs can exceed the cost of a proper redesign. For facilities planning capacity expansion or replacing problematic units, it is worth evaluating whether the storage system was specified around actual bulk solid properties. In larger projects, that consideration often becomes as important as tonnage, especially for installations using 800-1500 Tons Silos in sectors such as grain, building materials, power, and chemicals.
What operators should watch on every shift
Reliable discharge performance is usually protected by routine observation rather than occasional emergency response. The most useful shift-level checks are straightforward:
- Is discharge rate changing at the same feeder setting?
- Are there unusual sounds from the hopper or outlet area?
- Is manual intervention becoming more frequent?
- Do level readings match actual discharge behavior?
- Has weather or material source changed recently?
- Are dust emissions or venting behavior different from normal?
These observations may seem basic, but they are often what separate manageable flow issues from chronic plant problems. Dry bulk storage tanks do not fail only because of poor equipment. They fail operationally when small warning signs are normalized and the real cause is left unexamined.
For operators, the most effective mindset is to treat discharge behavior as a process condition that can be monitored, interpreted, and improved. Bridging, ratholing, surging, flushing, and buildup are not random annoyances. They are signals. When those signals are tied back to material condition, filling method, outlet performance, and maintenance history, prevention becomes much more practical—and far less costly than repeated downtime.
Related Posts
- ▶ How a Dry Bulk Silo Handles Pneumatic Filling and Gravity Discharge
- ▶ What Is a Dry Bulk Silo, and When Does a Factory Need One?
- ▶ Can dry bulk storage silos be integrated into existing PLC-controlled batching systems?
- ▶ Do dry bulk silos designed for API 650 compliance meet ASME Section VIII requirements?
- ▶ Is almacénamiento de sólidos a granel en silos de acero inoxidable viable for small-scale agrochemical distributors?
- ▶ How do vibration-based level sensors perform in stainless steel silos with powder coating?
Online Message