





Can stainless steel silos be welded onsite without compromising food-grade compliance?
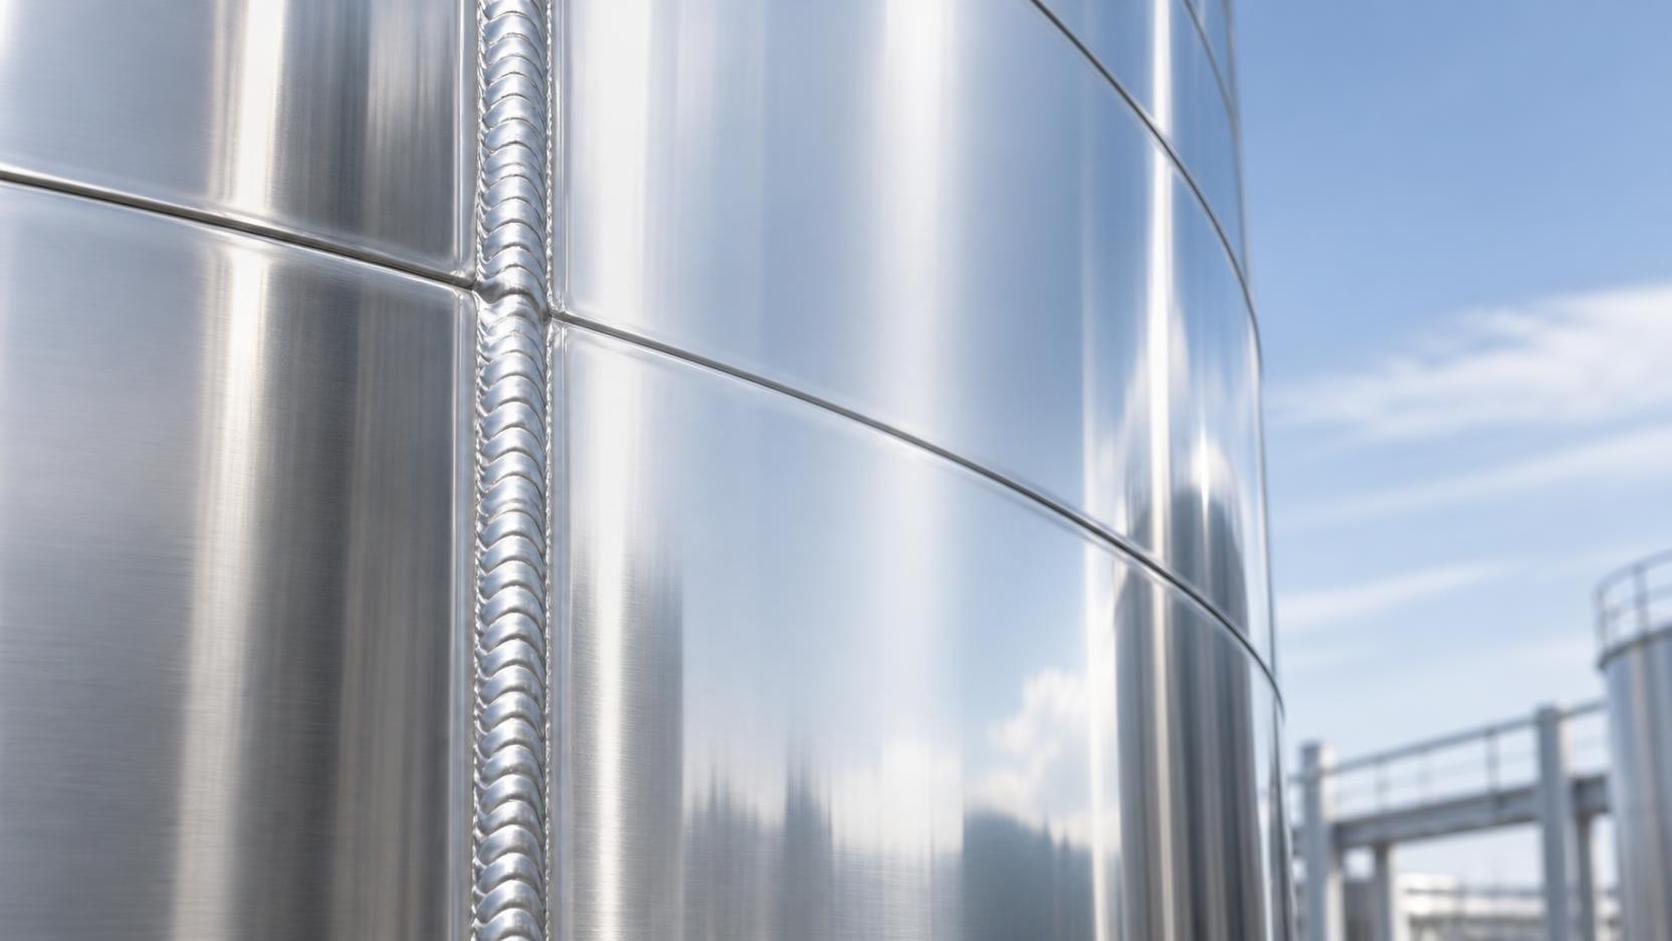
Yes—stainless steel silos can be welded onsite while maintaining full food-grade compliance, but only when strict material, procedural, and validation protocols are followed. For quality control and safety professionals overseeing food, pharmaceutical, or high-purity bulk storage projects, understanding the weldability, surface finish requirements (e.g., Ra ≤ 0.8 μm), and post-weld passivation standards of stainless steel silos is critical. Shandong Guokai International Trade Co., Ltd. leverages ISO-certified field welding teams, ASME-compliant procedures, and third-party verification to ensure every onsite weld meets FDA, 3-A, and EC 1935/2004 standards—without compromising hygiene, corrosion resistance, or structural integrity.
Onsite welding of stainless steel silos is not inherently noncompliant—but it shifts responsibility from factory-controlled fabrication to field-executed quality assurance. Unlike shop-welded units where environmental variables are tightly managed, field conditions introduce uncontrolled variables: ambient humidity, wind-borne particulates, temperature fluctuations, and operator consistency across shifts. These factors directly impact weld bead geometry, heat-affected zone (HAZ) width, and chromium oxide layer regeneration—all of which determine whether a weld remains inert, smooth, and microbially resistant.
The core issue lies not in *whether* welding can occur onsite, but *how* weld integrity is verified against food-grade criteria. FDA 21 CFR Part 110 and EC 1935/2004 do not prohibit field welding; they require that final surfaces meet defined thresholds for roughness, chemical composition, and passive layer performance. Specifically, Ra ≤ 0.8 μm is mandated for product-contact surfaces in dairy, infant formula, and sterile pharmaceutical applications—not as an arbitrary benchmark, but because surface irregularities exceeding this value trap organic residue, resist cleaning, and accelerate localized pitting under repeated CIP cycles. A weld that passes visual inspection and radiography may still fail microbial retention testing if its microfinish exceeds Ra 1.2 μm or contains embedded iron contamination.
Welding procedure specification (WPS) must therefore go beyond mechanical strength. It must define filler metal chemistry (e.g., ER316L with ≤ 0.02% carbon), interpass temperature limits (≤ 150°C to prevent sigma phase formation), shielding gas purity (≥ 99.998% argon with ≤ 3 ppm O₂), and post-weld dwell time before passivation. Field teams using generic “stainless steel” WPS templates often overlook that 304 vs. 316L base metals demand different heat input controls—and that grain boundary sensitization risk increases exponentially above 425°C for more than 30 seconds. Without real-time thermal monitoring and documented interpass cooling records, compliance cannot be objectively demonstrated.
Surface finish verification is equally non-negotiable. Ra measurement alone is insufficient. The FDA’s Guidance for Industry: Current Good Manufacturing Practice (CGMP) for Food notes that “surface texture must be assessed using calibrated profilometry at multiple points per weld seam, including root, cap, and heat-affected zones.” A single-point Ra reading on the weld crown does not reflect undercut or micro-crevices along the toe—common sites for biofilm nucleation. Third-party auditors routinely reject welds where profilometer traces show >15% deviation in peak-to-valley height across 1 mm sampling length, even if mean Ra is within spec. This level of granularity requires on-site metrology—not lab-submitted coupons.
Passivation is not a cosmetic step—it is the functional reset of the passive chromium oxide layer. ASTM A967 mandates nitric acid or citric acid passivation after welding, but food-grade applications require additional constraints: bath temperature must remain between 50–60°C (to avoid chloride stress cracking), immersion time must be validated per weld thickness and alloy (not fixed at 30 minutes), and post-passivation water rinse must achieve < 10 ppm total dissolved solids (TDS) to prevent flash rusting. Field passivation without conductivity meters, pH loggers, and TDS analyzers introduces unquantifiable risk. Residual chlorides left behind—even at 2 ppm—initiate crevice corrosion within 12 months under cyclic wet-dry exposure.
Documentation is the final gatekeeper. A compliant onsite weld package must include: certified welder ID cards with current qualification records (ASME Section IX QW-301), traceable filler wire lot numbers with mill test reports, thermal imaging logs per pass, profilometry reports signed by accredited metrologists, and third-party passivation validation certificates referencing ASTM A967 Method A or B. Generic “weld inspection reports” lacking these elements hold no weight during FDA pre-approval audits or 3-A Sanitary Standards certification reviews.
This rigor explains why some manufacturers refuse onsite welding outright—while others, like Shandong Guokai, integrate it into their certified delivery model. Their approach treats each field weld as a discrete validation event: pre-weld joint preparation is witnessed and photographed; interpass temperatures are logged via Bluetooth-enabled thermocouples synced to cloud-based QA dashboards; and every completed seam undergoes simultaneous profilometry and ferroxyl testing for free iron detection. No weld proceeds to next stage until all data points are approved by a designated quality engineer—not just the site supervisor.
For end users evaluating suppliers, the question isn’t “Can they weld onsite?” but “How do they prove each weld meets EC 1935/2004 Annex I migration limits for nickel and chromium?” Migration testing—required for any food-contact surface—must be conducted on actual welded samples, not base metal coupons. Suppliers who cite “material compliance” without providing migration test reports for welded joints are omitting the most consequential variable.
Field-welded stainless steel silos remain viable for food-grade applications—but only when treated as engineered systems, not fabricated structures. The Pellet Feed Steel Silo exemplifies this principle: designed for high-moisture, high-fat animal feed storage, its onsite assembly includes mandatory weld mapping, real-time HAZ temperature logging, and post-passivation electrochemical impedance spectroscopy to confirm oxide layer thickness ≥ 3 nm. Such protocols eliminate ambiguity—they convert regulatory language into measurable, repeatable, auditable actions.
Compliance isn’t achieved by selecting stainless steel—it’s sustained through controlled metallurgical transformation. Every onsite weld is a localized re-manufacturing event. Its success depends less on the skill of the welder than on the precision of the verification system surrounding them.
Related Posts
- ▶ How a Dry Bulk Silo Handles Pneumatic Filling and Gravity Discharge
- ▶ What Is a Dry Bulk Silo, and When Does a Factory Need One?
- ▶ Can dry bulk storage silos be integrated into existing PLC-controlled batching systems?
- ▶ Do dry bulk silos designed for API 650 compliance meet ASME Section VIII requirements?
- ▶ Is almacénamiento de sólidos a granel en silos de acero inoxidable viable for small-scale agrochemical distributors?
- ▶ How do vibration-based level sensors perform in stainless steel silos with powder coating?
Online Message